Home - tire valves - rubber tire valve - Page 2
As a premium rubber tire valve manufacturer, Fortune delivers OE-quality tire valve stems (including TR412, TR413, and TR600HP) for passenger cars, light trucks, and trailers. Backed by 30 years of expertise and an ISO/TS 16949 certified facility, our tyre valve stems utilize premium EPDM rubber and precision copper rods, ensuring perfect fitment for standard 11.5mm (.453″) and 16mm (.626″) rim holes. We provide global B2B buyers with 100% leak-tested schrader valves (withstanding up to 100psi), custom OEM specifications, and robust tire valve parts for the automotive aftermarket.
A reliable rubber tire valve requires application-specific engineering. Fortune delivers targeted solutions across all wheel categories: we utilize 100% EPDM to stop ozone cracking in passenger cars, reinforce copper stems for 100psi truck payloads, add high-temp cores for trailer storage, and guarantee OE dimensions for aftermarket fitment.
Every rubber tire valve requires exact rim fitment for optimal safety. As a comprehensive automotive manufacturer, Fortune engineers a full spectrum of tubeless tire valves and inner-tube solutions. From our high-volume rubber snap-in valves to specialized heavy-duty designs, we guarantee airtight seals and exact tolerances for standard .453″, wider .626″, and compact .346″ rim holes across all wheel applications.
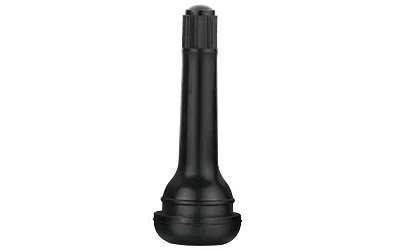
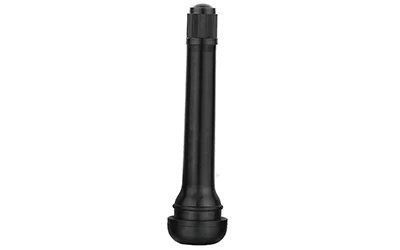
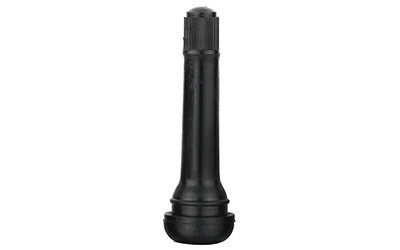
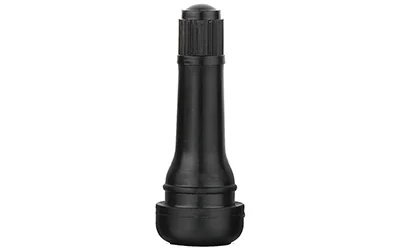
Our tire valve stems fit standard 11.5mm rim holes perfectly, serving as our primary auto valve solution for passenger cars. We design these high-quality tubeless tire valves with a 15mm base diameter to safely sustain a maximum cold inflating pressure of 65psi (450kPa). We equip each unit with a premium 9002# valve core and VC8 cap to ensure long-lasting air retention. Our comprehensive line of rubber snap-in valves includes the TR412 (22mm length), TR413 (30mm), TR414 (38mm), TR414L (45mm), and TR418 (49mm). For volume procurement, we provide our partners with full technical data sheets (TDS) detailing exact dimensional tolerances and material testing reports.
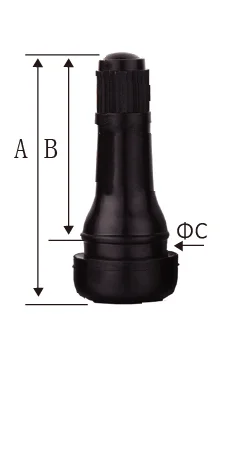
| MODEL NO. | RIM HOLE | EFF.LENGTH (MM) | CORE | CAP | A | B | C | PACKAGE |
| TR412 | Φ11.5/.453″ | 22 | 9002# | VC8 | 33 | 22 | 15 | 100 pcs/bag, 10 bags/case |
| TR413 | Φ11.5/.453″ | 30 | 9002# | VC8 | 42.5 | 32 | 15 | 100 pcs/bag, 10 bags/case |
| TR414 | Φ11.5/.453″ | 38 | 9002# | VC8 | 48.5 | 38 | 15 | 100 pcs/bag, 10 bags/case |
| TR414L | Φ11.5/.453″ | 45 | 9002# | VC8 | 56.5 | 46 | 15 | 100 pcs/bag, 10 bags/case |
| TR418 | Φ11.5/.453″ | 49 | 9002# | VC8 | 61.5 | 51 | 15 | 100 pcs/bag, 10 bags/case |
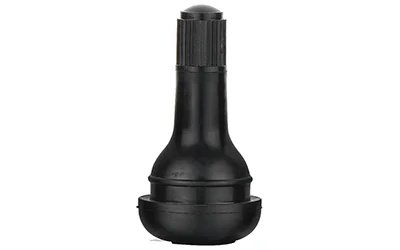
Our tyre valve solutions for 16mm (.626″) rim holes solve the sealing challenges of wide-aperture utility, agricultural, and older off-road wheels. We engineer these heavy duty tire valve stems with a reinforced 19.2mm base diameter to ensure an impenetrable fit within the larger rim cavity. This oversized rubber base physically prevents shear forces from breaking the seal, allowing the valve to safely sustain 65psi (450kPa) cold inflation pressure under harsh terrain conditions. To accommodate varying rim depths, we manufacture the TR415 with a standard 30mm effective length and the TR425 with an extended 49mm profile. Partner with us for ISO-certified, large-scale manufacturing of these specialized wide-base models.
| MODEL NO. | RIM HOLE | EFF.LENGTH (MM) | CORE | CAP | A | B | C | PACKAGE |
| TR415 | Φ16/.626″ | 30 | 9002# | VC8 | 42.5 | 32 | 19.2 | 100 pcs/bag, 10 bags/case |
| TR425 | Φ16/.626″ | 49 | 9002# | VC8 | 61.5 | 51 | 19.2 | 100 pcs/bag, 10 bags/case |
Our schrader valve TR438 series solves tight clearance issues for specialized 8.8mm (.346″) rim holes. We engineer these compact schrader valve stems with a minimized 11mm base diameter specifically for lightweight alloy and motorcycle wheels. The core advantage of this specialized fitment is structural preservation: smaller rim apertures maintain maximum wheel strength, while the valve’s compact 32mm effective length prevents dangerous high-speed protrusion and reduces rotational weight. To guarantee safety within this reduced profile, we strictly equip these assemblies with standard premium tire valve parts, including our high-temperature 9002# cores, ensuring a zero-leak seal in narrow spaces. Partner with us for precision-engineered, low-clearance valve solutions.
| MODEL NO. | RIM HOLE | EFF.LENGTH (MM) | CORE | CAP | A | B | C | PACKAGE |
| TR438 | Φ8.8/.346″ | 32 | 9002# | VC8 | 40.5 | 31 | 11 | 100 pcs/bag, 10 bags/case |
Commercial valve stems must sustain 100psi heavy cargo loads. We build these high pressure valve stems with a fully enclosed built-in copper structure to prevent base separation during severe commercial transport. Acting as top-tier truck tire valves, our products safely handle a maximum cold inflating pressure of 100psi (720kPa). We cover all your commercial needs by supplying the TR600HP (30mm) and TR602HP (49mm) for standard 11.5mm / .453″ rim holes, alongside the TR801HP (31mm) and TR802HP (49mm) for wider 16mm / .625″ rim holes. Partner with us to secure commercial-grade reliability through our factory-direct supply chain.
| TRNO. | EFF.LENGTH (MM) | Rim Hole | CORE | CAP | PACKAGE |
| TR600HP | 30 | Ø11.5 (.453″) | 9002# | VC8 | 100 pcs/bag, 10 bags/case |
| TR602HP | 49 | Ø11.5 (.453″) | 9002# | VC8 | 100 pcs/bag, 10 bags/case |
| TR801HP | 31 | Ø16 (.625″) | 9002# | VC8 | 100 pcs/bag, 10 bags/case |
| TR802HP | 49 | Ø16 (.625″) | 9002# | VC8 | 100 pcs/bag, 10 bags/case |
Every rubber tire valve must maintain a flawless seal under high-speed centrifugal forces and drastic temperature changes. Whether manufacturing high-volume tubeless snap-in models, heavy-duty commercial variants, or rubber-based tube valves, we utilize a fully enclosed built-in structure design. By permanently bonding 100% EPDM rubber to CNC-machined premium copper rods—and strictly eliminating brittle zinc alloys—we create a mechanically superior assembly guaranteed to survive the harshest driving environments. This same rubber-to-metal bonding technology underpins our rubber TPMS valves, engineered for direct sensor mounting.
Our rubber tire valves utilize high-quality EPDM instead of inferior natural rubber. Natural rubber easily ages in the air and frequently breaks during rim installation. We engineer our rubber base with 100% premium EPDM to provide superior resistance against ozone exposure, extreme weather, and chemical degradation. This material upgrade physically prevents the valve base from hardening, cracking, and leaking air over extended use.
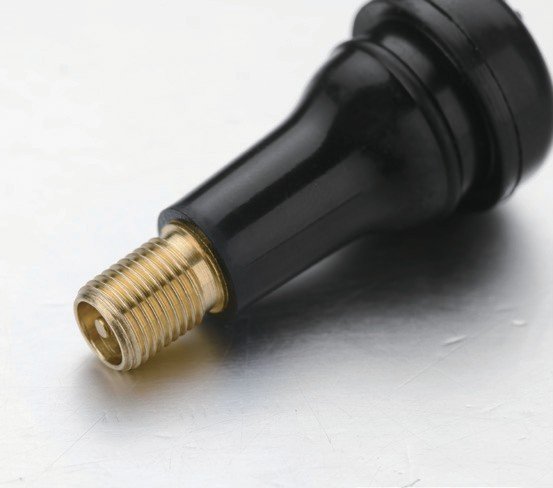
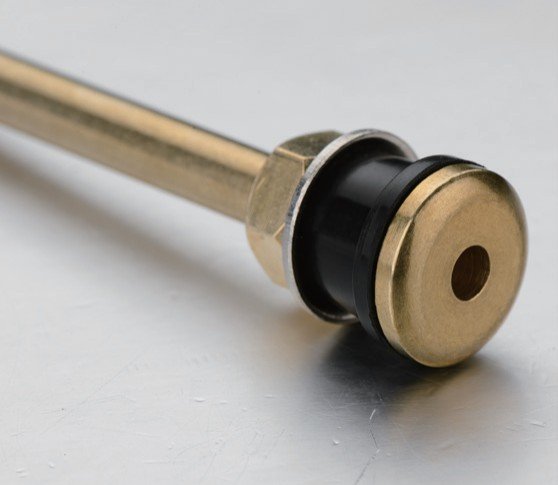
Inside our rubber valve stems, we completely replace zinc alloy and inferior metal compositions with high-purity copper. Low-cost market alternatives utilize zinc alloy main rods that suffer from poor sealability and unstable material properties, resulting in premature cracking, aging, and a high risk of failure under mounting stress. In contrast, we produce our internal stems exclusively using advanced CNC processing machinery to achieve high precision and smooth surfaces. This precision manufacturing guarantees exact dimensional tolerances and a secure rubber-to-metal bonding interface that withstands installation forces and high-speed operational loads without structural shear.
Premium tire valve parts dictate the air retention capabilities of the entire assembly. We equip our rubber valves with a full spectrum of cores to match your exact working environment. While our flagship 9002# high/low-temperature core (identifiable by its red gasket) flawlessly sustains extreme ranges from -54°C to +150°C, we also manufacture the standard 9001# black gasket series (-40°C to +100°C), freon-resistant cores (9005#/9006#), and specialized gas-resistant options.
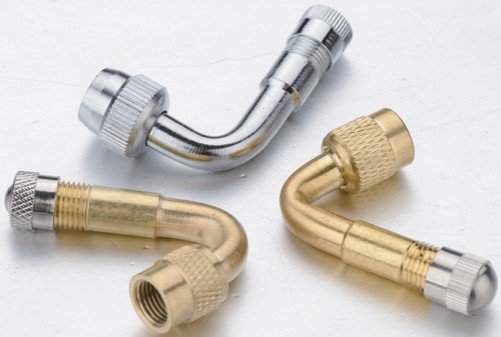
Our rubber tyre valve assemblies rely on functional caps with built-in internal sealing rings to physically block dirt, water, and salt corrosion from reaching the core. We manufacture the standard VC2, VC3, and FT series in premium brass, alongside the VC-P series in durable plastic and the VC-A series in customizable aluminum. To accommodate varying deep-dish wheel profiles, our extension catalog provides exact dimensional configurations: 13mm to 32mm extensions for passenger cars, rigid metal truck extensions ranging from 40mm to 142mm, and flexible rubber extensions up to 300mm in total length.
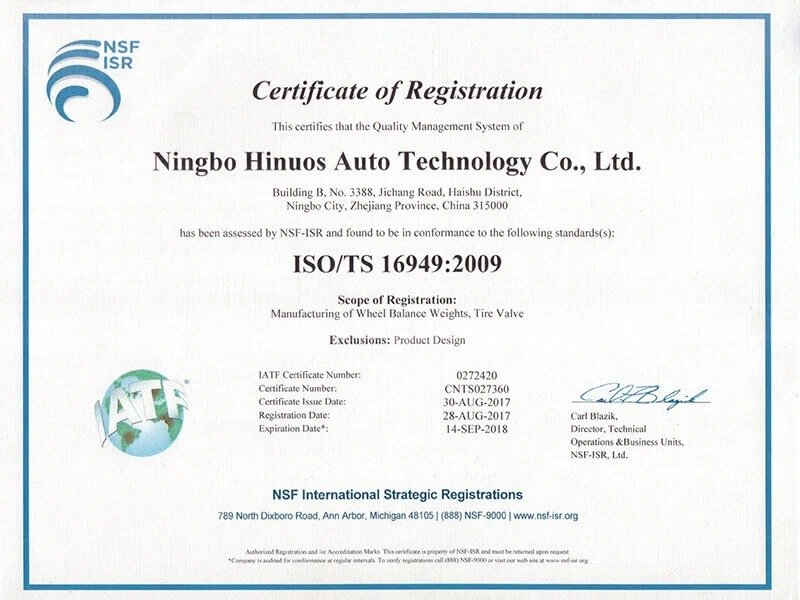
Every rubber tire valve we produce undergoes rigorous inspection to ensure absolute safety and performance. Founded in 1996, our facility operates under the core principle of “To develop with technology and to survive with quality,” fully backed by our TÜV SÜD-certified ISO/TS 16949 quality management system. Supported by an experienced team of over thirty engineers and automated testing laboratories, we consistently deliver zero-defect tire valves, including every reliable car tyre valve and heavy-duty truck tire valve stems, to OEM and aftermarket partners across the Americas, Europe, Japan, Asia, and Oceania.
01
Every tire air valve undergoes strict 100% automated leakage testing before leaving our production line. To guarantee flawless sealability, each assembly is subjected to high-pressure pneumatic leak detection, safely testing the internal core up to 15 kgf/cm² (212 psi). Because a faulty valve can cause rapid tire deflation, we utilize precision pressure decay sensors to verify that absolutely no micro-leaks exist between the copper rod and the rubber housing. This mandatory diagnostic step guarantees that whether you are sourcing standard passenger car models, 100-psi heavy-duty truck tire valve stems, or specialized motorcycle valve units, the internal core and base will never leak under extreme operational pressure.
02
Heavy rubber valve stems must survive extreme mechanical stress, particularly the severe pull-in friction during rim installation and continuous high-speed centrifugal forces. We utilize computerized tensile testing machinery to physically measure the ultimate yield strength between the EPDM rubber housing and the internal CNC-machined copper core. By clamping the metal stem and applying intense destructive pull-force, we verify that the rubber-to-metal bonding interface withstands maximum Newton (N) shear thresholds before any separation occurs. This exact metric confirms that our tyre valve stems will not shear, crack, or detach—even when mechanically forced through tight .453″ (11.5mm) or .625″ (16mm) rim holes or subjected to severe commercial road vibrations.
03
All tubeless valves face severe environmental degradation, as standard natural rubber easily ages in atmospheric oxygen and frequently breaks during rim installation. To validate our international high-standard EPDM formulation, we subject our products to accelerated dynamic ozone aging chambers. By placing the rubber exterior under continuous physical tension (elongation) while exposing it to highly concentrated ozone levels and elevated temperatures, we simulate years of severe UV and harsh environmental exposure in mere days. This destructive aging simulation confirms our EPDM compound will never exhibit the hardening, micro-cracking, and rapid chemical breakdown associated with inferior materials. Even in rugged applications requiring robust atv valve stems or off road valve stems, our assemblies guarantee long-term flexibility and weather resistance.
04
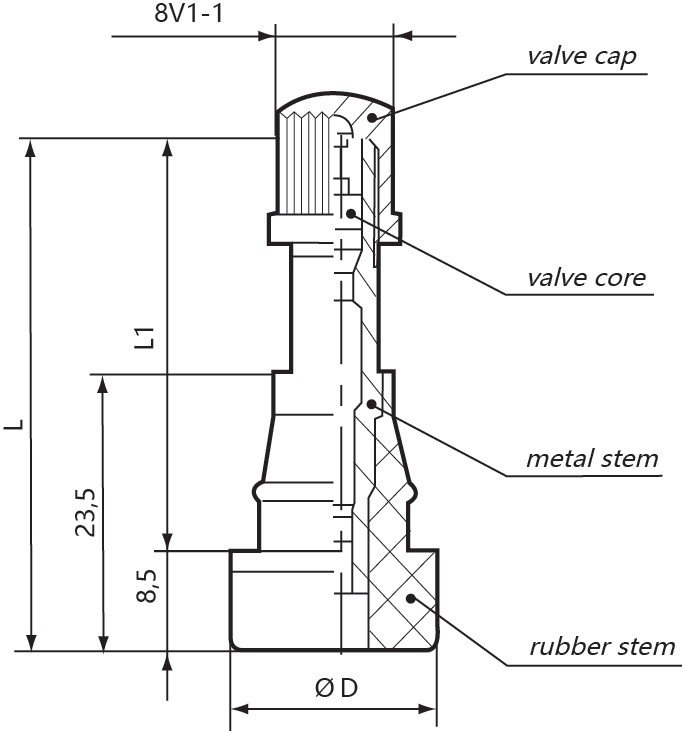
Our wheel valve stems demand exact engineering tolerances to achieve the critical interference fit required for a blowout-proof seal. Our quality control technicians utilize high-precision optical comparators and micrometer calipers to strictly verify exact batch dimensions against our technical drawings. We specifically measure the critical sealing zones—such as verifying the exact 15mm rubber base diameter designed to compress into standard .453″ (11.5mm) rim holes, and the wider 19.2mm base for heavy-duty .626″ (16mm) applications. Furthermore, we meticulously inspect the effective lengths (ranging from the 30mm TR413 to the 49mm TR418) and validate the precise 8V1-1 internal core threading. This strict dimensional validation guarantees that every car tyre valve seats flawlessly without dangerous micro-gaps, eliminating the risk of pressure loss during high-speed cornering.
05
New tire valve parts and incoming raw materials face uncompromising metallurgical and chemical laboratory scrutiny before ever entering our assembly lines. We conduct thorough formulation analysis on our rubber batches to guarantee a 100% premium EPDM composition, strictly detecting and rejecting any inferior natural rubber blends or cheap fillers that cause premature aging and cracking. For our metallic components, we utilize rigorous comparative laboratory salt-spray testing on our CNC-machined premium copper rods and brass assemblies. This accelerated environmental testing confirms our components maintain a pristine, rust-free surface, completely outperforming cheap zinc-alloy alternatives that rapidly oxidize and structurally weaken under harsh road-salt conditions. By auditing material purity right at the source, we ensure every finished product strictly complies with the ISO/TS 16949 OE requirements demanded by our global distributors.
Every rubber tire valve we manufacture can be engineered down to the precise millimeter and chemical compound to match your exact OEM specifications. Backed by an experienced R&D team of over thirty engineers, we move beyond generic supply to offer comprehensive ODM capabilities. Whether your private-label project requires modifying effective stem lengths (from a compact 30mm TR413 to an extended 62mm TR423), adapting base diameters for standard .453″ (11.5mm) or heavy-duty .626″ (16mm) rim holes, or integrating freon-resistant 9005# cores and custom-color aluminum caps, we execute your technical blueprints flawlessly. From rapid prototyping of bespoke tooling to delivering retail-ready blister packaging, we partner with global distributors to build highly competitive, exclusive product lines.
Specialized rubber tire valve orders frequently demand micrometer-level precision to guarantee a blowout-proof interference fit on unique wheel rim profiles. Moving beyond standard catalog sizes, our OEM engineering team customizes the internal brass stem geometries, exact rubber base diameters, and pull-in resistance thresholds to accommodate non-standard rims. Whether your portfolio requires the ultra-compact 30mm effective length of a TR413 (featuring a precise 15mm rubber base to perfectly seal a .453" / 11.5mm rim hole), or the extended 62mm TR423 designed with a 19.2mm base for heavy-duty .625" (16mm) commercial applications, we execute your technical blueprints flawlessly. We utilize multi-axis CNC turning centers to machine the internal copper rods and standard 8V1-1 core threads to strict ±0.02mm tolerances, while our custom injection molds strictly control the EPDM rubber compression ratios for high-speed dynamic sealing.
Premium rubber valve stems must survive the specific climatic challenges of your target geographic market, from -40°C winter freezes to continuous +100°C operational heat. While our standard assemblies utilize 100% premium EPDM—proven to pass strict 72-hour / 50 pphm accelerated ozone chamber tests without micro-cracking—our chemical laboratory can fine-tune the compounding formula for bespoke orders. If your commercial fleet operates in extreme sub-zero territories (down to -54°C) or high-UV off-road environments, we precisely adjust the elastomer blend, carbon black ratios, and Shore A hardness. This exact chemical engineering ensures the housing remains perfectly pliable without structural hardening, guaranteeing that its critical compression set and interference fit inside a .453" rim hole remain 100% airtight under severe dynamic loads.
Unique tire valve parts dictate both the secondary sealing reliability and the visual branding of your assemblies. Moving beyond generic components, we offer complete micro-level customization for the internal 8V1 core chamber. You can select specific precision-engineered valve cores: the standard 9001# equipped with standard black seals, the extreme-temperature 9002# utilizing red high-grade cup seals to safely withstand -54°C to +150°C, or the 9005# variants engineered with specialized O-rings for strict freon resistance. Externally, you can fully configure the protective valve caps across our VC-A (anodized aluminum), VC-P (injection-molded durable plastic), or heavy-duty CNC-machined brass series. To guarantee a blowout-proof secondary seal against micro-leaks and road salt, we specifically integrate premium EPDM sealing gaskets directly inside our metal caps. Furthermore, we support precise Pantone color matching and high-resolution laser-etched corporate logos on the metallic cap surfaces, delivering a premium, retail-ready finish that perfectly matches your branding.
Retail wheel valve distribution and bulk industrial supply require drastically different logistical presentations. For bulk OEM clients, we utilize heavy-duty 5-ply corrugated export cartons and moisture-proof, heat-sealed PE bags (e.g., strictly 100 pcs/bag) to maximize sea-freight container efficiency and prevent transit damage. For aftermarket brands, we provide high-end, shelf-ready retail solutions. You can choose from CMYK offset-printed color boxes with custom UV coatings, or high-clarity PET blister packages featuring tamper-evident sealing and integrated EAN/UPC retail barcodes. To permanently eliminate dispatch discrepancies, our packaging lines utilize high-precision electronic weight-checking scales and optical scanners during the final in-line inspection. This zero-tolerance fulfillment protocol ensures your customized inventory arrives flawlessly presented, perfectly palletized, and 100% accurate for immediate warehouse distribution.
With 30 years of dedicated manufacturing expertise, Fortune is a premier source factory specializing in high-volume tire valve production. We currently export to over 50 countries across North America, Europe, and Asia, serving top-tier automotive aftermarket distributors. Backed by an in-house R&D team of 30+ engineers and strict TÜV SÜD ISO/TS 16949 quality certification, we control the entire process from raw material compounding to final assembly. By providing direct-to-factory OEM services, 24/7 technical support, and localized logistics through our North American branches, we guarantee zero-defect quality and secure global fulfillment.
With exactly 30 years of deep industry accumulation, we produce high-volume tire valves for top-tier aftermarket brands. Our products are widely exported to over 50 countries, spanning major markets across North America, Europe, and Asia.
We operate under the strictest international automotive quality management systems. Fully certified by TÜV SÜD ISO/TS 16949, we guarantee 100% traceability and zero-defect quality control throughout the entire manufacturing process.
Backed by an in-house R&D team of over 30 engineers, we independently handle everything from raw material compounding to mold processing. This allows us to rapidly develop and customize any standard or specialized tire valve products.
We eliminate middlemen to provide highly efficient, factory-direct OEM/ODM services. Supported by our dedicated North American branches and warehouses since 2014, we deliver rapid localized logistics, flexible inventory, and 24/7 technical support.
Acorn lug nuts that are not tightened to the correct torque can cause a wheel to come loose at highway speed — one of the most dangerous failures a driver can experience. Too loose, and the wheel works free over the first 100 km; too tight, and the studs stretch
Lug nuts with incorrect torque can cause a wheel to come loose at highway speed — one of the most dangerous failures a driver can experience. Too loose, and the wheel works free over the first 100 km; too tight, and the studs stretch or snap under load. The fix
A wheel comes off the balancer with a 0.25 oz imbalance marked at the 6 o’clock position. The operator cleans the spot, presses on an adhesive wheel weights strip, watches the display drop to zero, and rolls the wheel to the mounting rack — only to find the weight sitting
The stock wheel nuts on most cars do their work without anyone noticing them — until the day a wheel wobbles, a stud snaps, or a finish gets scratched during a tire swap. Aftermarket lug nuts solve the cosmetic problem but introduce a technical one: every wheel and stud combination
Yes. We manufacture tens of millions of standard snap-in rubber valves monthly. Driven by 60+ automated vacuum vulcanization presses, we maintain continuous high-volume production for all standard TR models. We execute global dispatch for full-container bulk orders within a strict 7 to 10-day window.
Yes. While standard passenger vehicles operate reliably on our Natural Rubber compounds, we independently formulate severe-weather EPDM for extreme environments. If your fleet operates in Arctic cold or continuous high heat, we calibrate the Shore A hardness to guarantee structural pliability at -40°C and zero cracking during 72-hour high-concentration ozone chamber tests.
Yes. Our entire rubber valve production line is governed by ISO/TS16949:2016 standards. Every batch strictly complies with SAE J1205/J1206 and TUV/DOT requirements. We do not rely on statistical batch sampling—100% of our outgoing rubber valves must pass through automated pneumatic leak testers before entering the VCI packaging phase.
Submit your volume requirements, target TR model, or specific OEM dimensions (e.g., custom base diameters or core lengths). We provide direct factory wholesale pricing within 24 hours. If you require a custom rubber valve design, our in-house tool-and-die center will fabricate the mold and dispatch functional prototypes for fitment testing within 48 to 72 hours.
We control the physical bonding surface. Our in-house CNC centers machine the HPb59-1 brass cores to a precise Ra 0.4 µm roughness to maximize mechanical adhesion. During the automated thermal curing process, we eliminate internal porosity. We validate this structural integrity through >600N axial pull-out force testing, mathematically eliminating base separation risks.