Home - tire valves
As a top tire valves manufacturer with 30 years of dedicated manufacturing experience, we supply global OEMs and aftermarket distributors with 100% leak-tested rubber snap-in and CNC-machined metal clamp-in valve stems, leveraging our ISO/TS 16949 certified facility, premium EPDM rubber, and solid copper construction to deliver exceptional sealability and ultimate driving safety across all passenger and commercial vehicle applications.
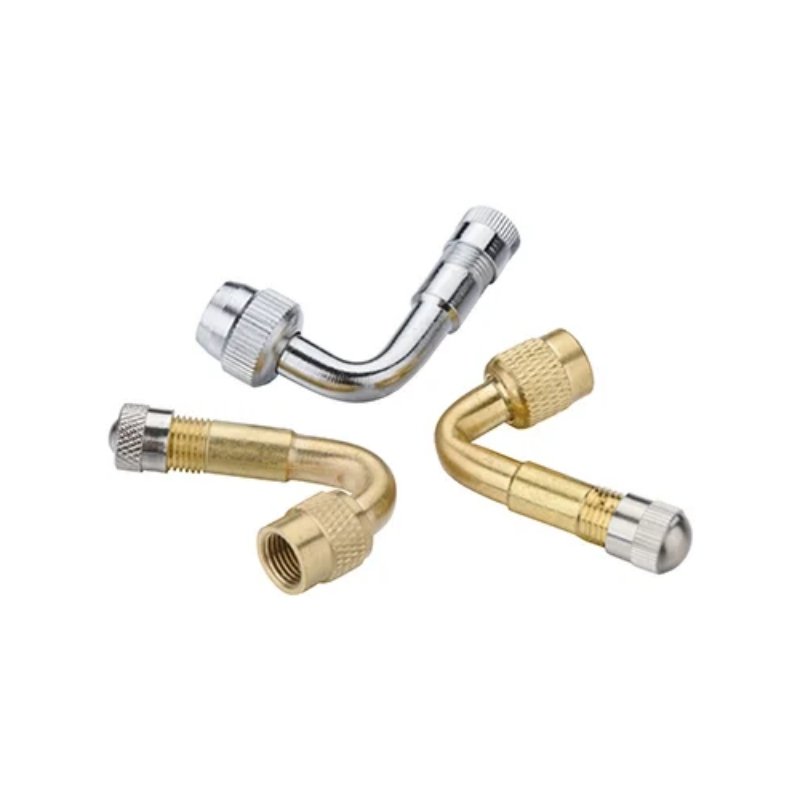
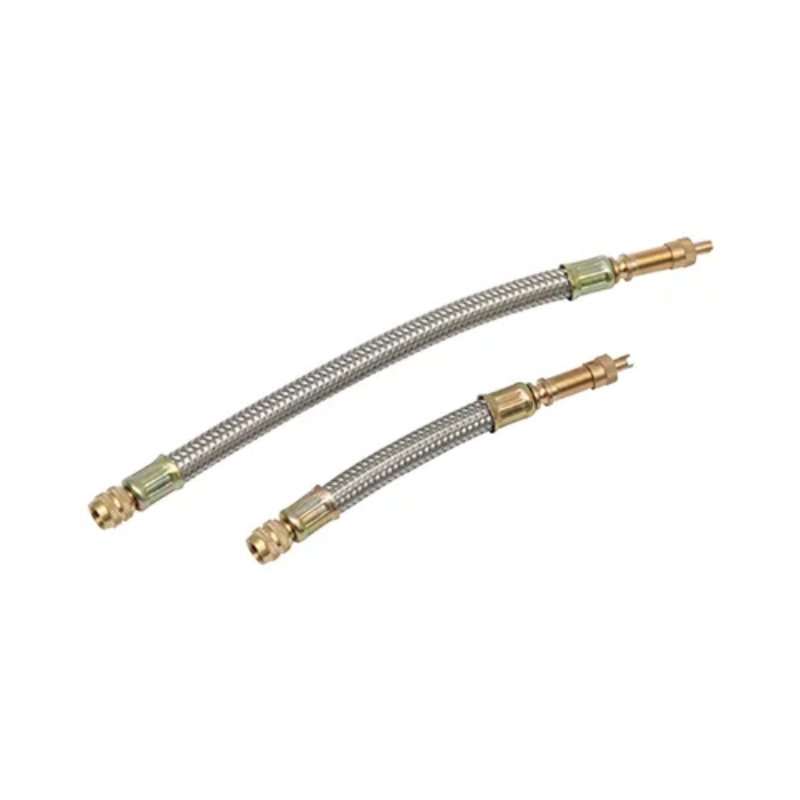
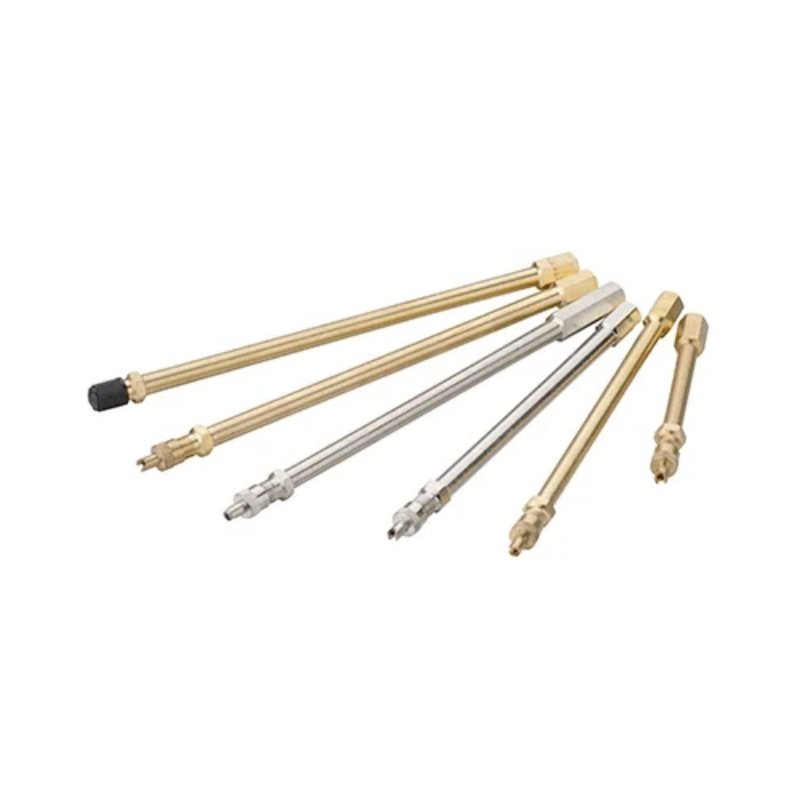
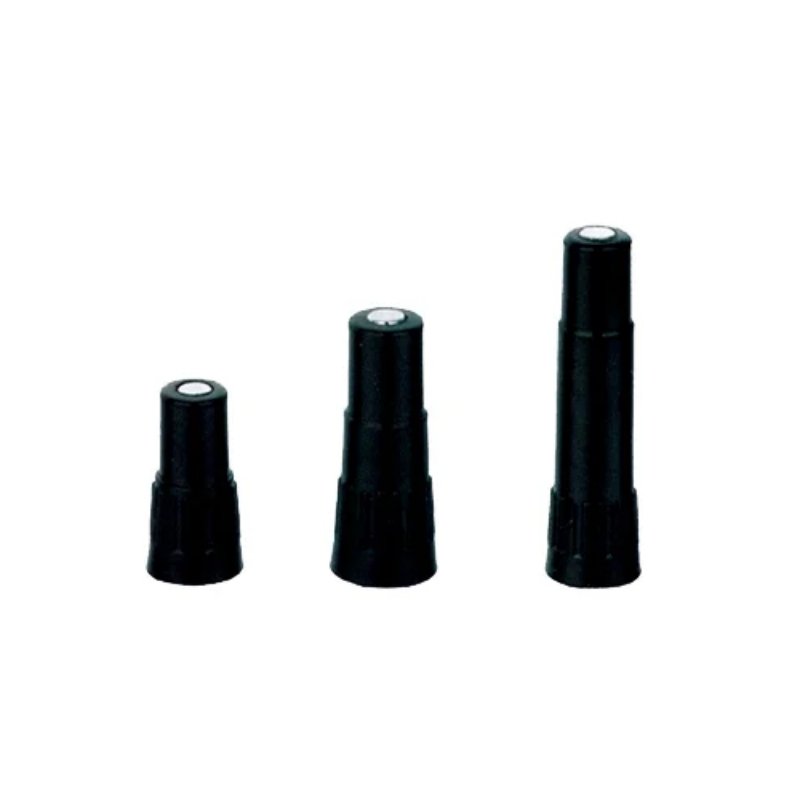
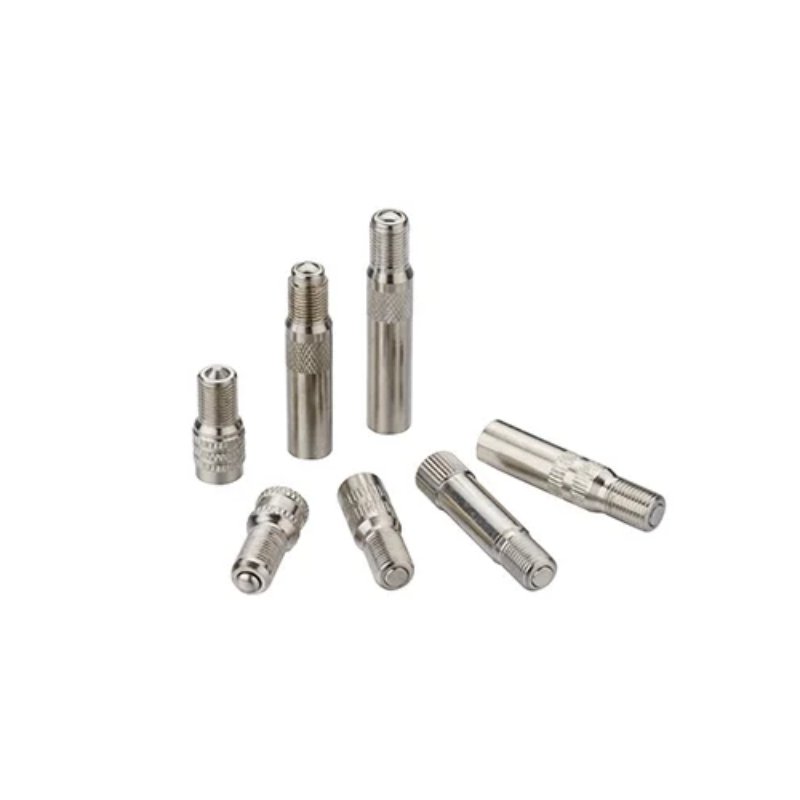
Matching the tire valve material to the specific operational environment is critical. We categorize our primary tire valves into two core materials: rubber and metal. To ensure sealing reliability, our valves utilize high-performance components like the 9002# valve core, preventing air leakage in extreme temperatures from -54°C to +150°C. Whether the application requires standard 65 PSI (450 kPa) cold inflation pressure or heavy-duty mechanical clamping, this material-based classification helps you quickly identify the exact specifications needed.
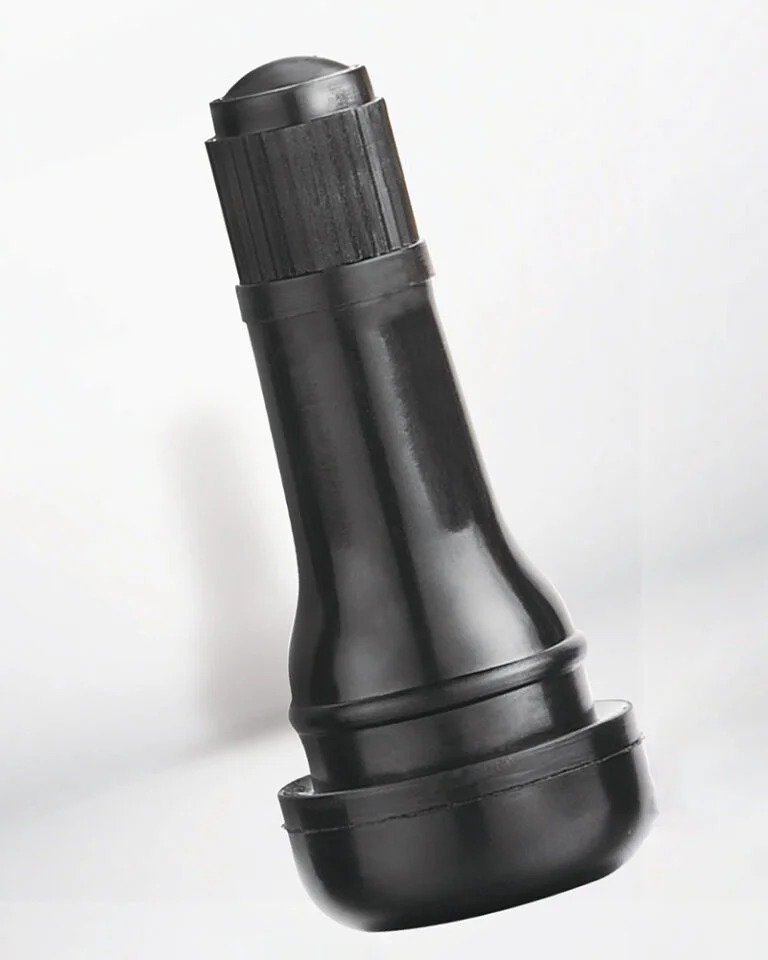
Manufactured to exact OE standards, our rubber tire valve series utilizes premium EPDM rubber combined with a robust core to resist ozone degradation and premature aging. Engineered specifically for standard Ø11.5 mm (0.453″) and Ø16 mm (0.625″) rim holes, these rubber snap in valve stems deliver precise sealing performance for automotive assembly lines and repair shops.
We supply a comprehensive range of snap-in tubeless tire valves. Our standard series, including TR412 valve stems (22mm effective length), TR413 tire valves (30mm), and TR414 valves (38mm), are rated for a max cold inflating pressure of 450 kPa/65 psi at room temperature. For heavy-duty commercial applications, our high-pressure tire valve stems, such as the TR600HP tire valve, can safely handle up to 720 kPa/100 psi.
Every rubber tubeless valve comes pre-assembled with our reliable 9002# schrader valve core and a standard VC8 cap, ensuring quick, tool-assisted insertion into the rim without the risk of core damage.
Sourcing bulk rubber tire valve stems directly from our factory ensures predictable cost-control. Whether you are ordering a standard tubeless car tire valve or a high-volume rubber wheel valve, our 100% automated leak testing guarantees consistent air retention across every batch.
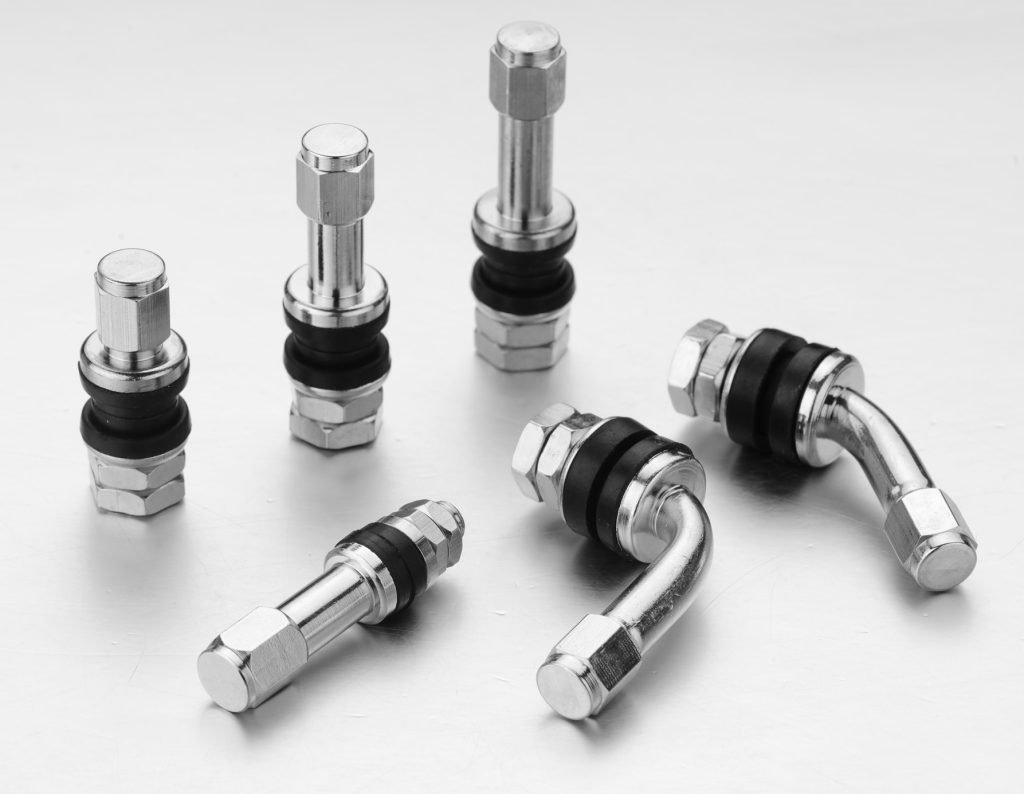
When wheel specifications demand higher mechanical strength, our metal tire valve solutions deliver precise structural integrity. Rather than relying on rubber friction, these metal valve stems lock into standard Ø11.5mm (0.453″) and Ø16mm (0.625″) rim holes using specified threaded hex nuts (such as HN4 and HN13) paired with custom rubber grommets (including RG54 and RG15). For commercial transport and high-pressure applications, we also utilize advanced O-ring sealing structures (found in our V3.20 metric and TR540 series) to create a watertight, high-torque fitment built to withstand severe environmental stress and heavy fleet payloads.
Our metal catalog extends far beyond standard passenger applications. While we supply premium clamp in valve and bolt in tire valve stems (like the MS525 series and TR416) for standard cars, we also manufacture a complete line of commercial truck tire valve stems. This includes the heavy-duty TR500 straight valve series, TR570 bent valves, and V3.20 European style O-ring seal brass valves designed for heavy payloads and fleet transport.
To meet diverse environmental and application needs, we engineer our metal tire valve stems in various premium materials. Procurement teams can specify a heavy-duty brass tire valve for commercial trucks, a lightweight aluminum tire valve for custom alloy wheel valve stems, or a treated chrome tire valve for aftermarket passenger vehicle styling.
Sourcing our extensive metal series guarantees reliable mechanical fixation under verified industrial stresses. Whether you require a standard metal schrader valve for passenger alloys, or a heavy-duty brass truck valve engineered to withstand commercial tire pressures up to 14 Bar, our production delivers exact tolerances. Our CNC machining ensures flawless thread pitches and precise stem angles—including straight, 27°, 45°, and 90° bends found in our TR570C and VS-8 series—guaranteeing accessible inflation points for complex dual-wheel fleet setups while completely eliminating the risk of high-pressure valve blowout.
Supplying reliable tire valves and valve stems requires matching exact PSI limits and rim dimensions. We engineer targeted solutions for distinct vehicle demands. By optimizing 65 PSI (450 kPa) rubber compounds for passenger cars, manufacturing metal housings rated for 14 Bar commercial truck pressures, and CNC-machining 90° bends for tight motorcycle clearances, our factory directly solves your fitment challenges. Whether you need a standard wheel valve for a 0.453″ rim hole or a specialized auto schrader valve for a Ø8.3 mm motorcycle rim, we deliver precise configurations for your distribution network.
01
Scenario Challenge: High-volume automotive assembly and aftermarket repairs demand valves that install in seconds but guarantee zero air leakage under continuous driving friction. Premium alloy wheels also present the challenge of high-speed centrifugal deflection, requiring strict material compliance to avoid premature aging or valve blowout.
Targeted Solutions: Manufactured strictly under our ISO/TS 16949:2018 certified quality management system, our rubber snap in tire valve stems are molded from international high-standard EPDM rubber to prevent ozone degradation and weather-induced cracking. These tubeless car tire valve assemblies utilize the precision 9002# car schrader valve core, which securely prevents air loss in extreme temperatures ranging from -54°C to +150°C, and are officially rated for a maximum cold inflation pressure of 65 PSI (450 kPa). To solve centrifugal deflection on premium rims, our metal car tubeless tyre valve assemblies undergo strict salt-spray lab testing to ensure superior corrosion resistance and provide rigid mechanical fixation.
Product Capabilities: For standard universal Ø11.5mm (0.453″) rim holes, distributors rely on our core tr412 valve stems, tr413 tire valve, and tr414 tyre valve production lines. For custom alloys, we supply the MS525 metal series. Whether your inventory requires a standard car wheel tire valve, a sleek alloy tubeless valve, or bulk car tire valve stems, we deliver exact fitments backed by rigorous laboratory validation.
02
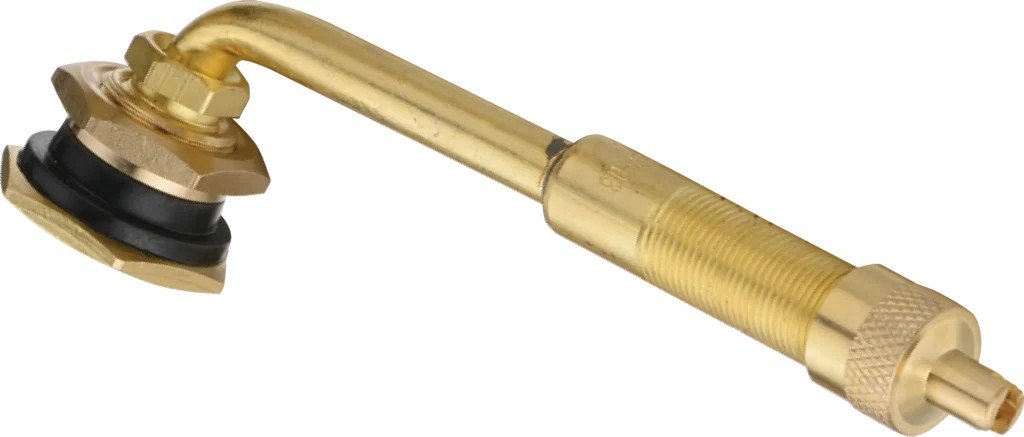
Scenario Challenge: Heavy-duty commercial fleets and transport rigs face extreme load-bearing stress, constant high-speed friction, and elevated tire temperatures. Standard valves risk catastrophic blowouts under these high-tonnage environments, making robust mechanical fixation and extreme high-pressure retention absolutely critical for fleet safety.
Targeted Solutions: Backed by our ISO/TS 16949:2018 manufacturing standards, we reinforce the structural integrity of our heavy duty tire valve stems using premium copper rods and CNC processing to ensure flawless thread pitches and absolute sealing. For light commercial vans, our high pressure tire valve stems utilize a thickened EPDM rubber base to safely manage continuous cold inflation up to 100 PSI (720 kPa). For heavy-duty transport rigs, our metal bolt in valve stems are engineered with secure threaded hex nuts and premium rubber grommets to physically lock into the rim, officially rated for extreme commercial tire pressures up to 14 Bar.
Product Capabilities: For standard Ø11.5 mm (0.453″) and Ø16 mm (0.625″) rim holes, we supply the tr600hp valve stems and tr600hp tire valve series. For maximum tonnage, our heavy duty truck valves—including the TR500 straight series, TR540 bent series, and specialized TKTV clamp in truck valves—completely eliminate blowout risks. When you source our brass truck tire valve stems or a general truck tyre valve, you guarantee strict quality control and minimize maintenance downtime for global fleets.
03
Scenario Challenge: Two-wheeled and off-road vehicles present severe installation constraints, characterized by highly compact rim clearances and hard-to-reach inflation points. Furthermore, ATV and off-road applications demand high resistance to impact, mud, and corrosive elements, requiring specialized materials that will not snap or leak under severe vibration.
Targeted Solutions: To solve accessibility issues without compromising sealing, we engineered the PVR tubeless series, utilizing premium ozone-resistant rubber compounds and featuring a specialized 90 degree tire valve stems structure. This specific 90 degree motorcycle valve stems design allows end-users easy inflation access on tight rims while securely sealing standard Ø11.5 mm holes against vibration leaks. For rigid metal solutions, our valves undergo strict salt-spray lab testing to guarantee long-lasting anti-corrosion performance in exposed off-road conditions.
Product Capabilities: Beyond rubber solutions, we solve the challenge of restrictive motorcycle rims with the MVA31 metal motorcycle tubeless tyre valve, which is precisely CNC-machined to fit much smaller Ø8.3mm and Ø11.3mm rim holes. From a flexible motorcycle tire air valve and rigid motorcycle wheel valve to durable off road tire valve stems for ATVs, we engineer the exact clearances and structural durability your customers demand.
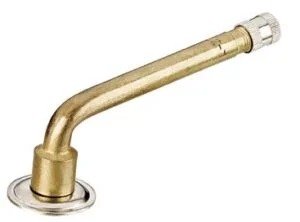
A premium tire valve must precisely match the wheel’s rim hole dimensions and peak inflation limits. We engineer our wheel tire valve production across three distinct structural categories: Snap-in, Clamp-in, and High Pressure. Whether your assembly line demands a flexible push-through tubeless stem for a standard Ø11.5mm (0.453″) rim, or a threaded tire schrader valve mechanically locked down with an HN4 hex nut, this structural focus ensures procurement teams source the exact physical fitment required to prevent high-speed deflection and blowouts.
Distributors sourcing complete wheel service programs often pair our valves with wheel balance weights for a single, reliable supplier relationship.
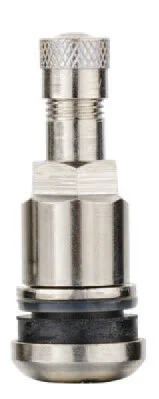
Our snap in valves are engineered with a flexible EPDM rubber body molded over a rigid brass or aluminum core. Rather than using mechanical fasteners, this structure utilizes rubber elasticity. During installation, the rubber snap in tire valve is pulled through the rim hole using a pneumatic lever tool. The rubber base safely compresses under standard 180N to 400N pulling forces and immediately expands, forming a self-sealing, airtight friction fitment without tearing the rubber housing.
Designed for rapid, tool-assisted push-through assembly. By completely eliminating threaded nuts and manual torque calibration, this snap-in structure reduces installation time to under 3 seconds per wheel—saving approximately 80% to 85% of assembly labor time compared to traditional mechanical clamp-in alternatives.
Rigorously tested to maintain a maximum cold inflating pressure of 65 PSI (450 kPa) at room temperature, while the internal 9002# valve core guarantees sealing stability in extreme temperatures ranging from -54°C to +150°C.
Our snap in tire valve stems accurately accommodate universal Ø11.5 mm (0.453") and Ø16 mm (0.625") rim holes. The core production line includes the 22mm tr412 valve stems, the 30mm tr413 tire valve, and the 38mm tr414 tyre valve. Whether distributing standard tubeless tire stems or a generic rubber snap in wheel valve, this structure delivers unmatched cost and time efficiency for high-volume automotive assembly.
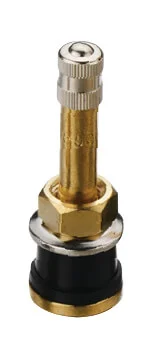
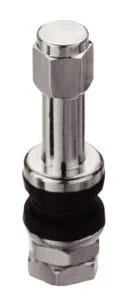
Unlike flexible snap-in models, a clamp in tubeless valve provides absolute mechanical fixation. These bolt in valve assemblies feature a rigid metal body that fastens securely to the wheel. The airtight seal is created by compressing a precision rubber grommet (such as our RG54 or RG39 models) against the rim using a threaded hex nut (like the HN4 or HN9) tightened to a recommended installation torque of 4 to 6 N·m (Newton-meters).
By eliminating reliance on rubber friction, these bolt in tire valve stems will not flex, deflect, or dislodge under extreme centrifugal forces generated by heavy custom alloys or high-speed driving up to 250 km/h (155 mph).
Engineered to create a watertight, high-torque fitment capable of withstanding severe radial loads and high-pressure differentials for both standard Ø11.5mm (0.453") and Ø16mm (0.625") rim holes.
We manufacture specialized metal bolt in valve stems tailored to precise fleet and aftermarket demands. This lineup features the MS525 series, which provides precision-machined brass and aluminum bodies designed for high-end passenger and sports alloy wheels requiring low-profile clearance and high-speed stability, alongside the TR416 clamp-in series, which offers heavy-duty agricultural and commercial configurations engineered for Ø16mm (0.625") rim holes with extended thread lengths and reinforced hex nuts for high-torque mounting. Whether sourcing rigid clamp in truck valves or passenger wheel stems, our advanced CNC machining delivers exact thread pitches, such as standard 0.305"-32 threads, ensuring seamless compatibility with standard tire pressure monitoring systems (TPMS) and extension adapters.
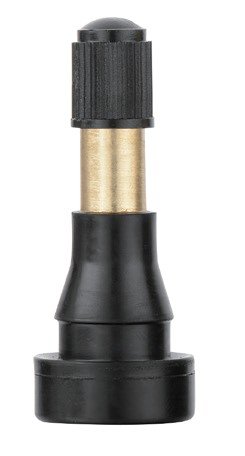
Our high pressure valve stems combine the fast-assembly convenience of a snap-in structure with the heavy-duty pressure retention of a commercial valve. We structurally reinforce these tubeless tire stem designs by increasing the EPDM rubber base thickness by 35% compared to standard passenger models and integrating a CNC-machined, high-tensile brass core (such as HPb59-1) to withstand intense internal air expansion and severe radial loads.
The reinforced base features a precisely calibrated 65±5 Shore A rubber hardness and an expanded 19mm anti-extrusion bottom collar. This exact geometric engineering ensures the heavy duty valve stems withstand over 600N of axial pull-out force. It actively prevents the valve from being pushed out or blowing out of the rim hole when subjected to the high-frequency wheel vibrations and continuous 100°C thermal expansion environments required by Class-3 commercial light trucks and heavy transport vans.
Rigorously lab-tested to safely manage a maximum continuous cold inflating pressure of 100 PSI (720 kPa) at room temperature. Equipped with a precision 9002# valve core, it provides stable, zero-leak air retention under sustained highway hauling conditions, featuring a tested operational temperature tolerance ranging from -40°C to +100°C and proven ozone resistance.
Our high pressure tire valve lineup includes the 30mm tr600hp valve stems and tr600hp tire valve precisely molded for standard 0.453" (11.5mm) holes, alongside the TR801HP engineered for larger 0.625" (16mm) commercial rim holes. Machined with standard 0.305"-32 threads for seamless TPMS and extension compatibility, this design delivers ultimate commercial-grade safety for bulk fleet sourcing.
Catastrophic tire blowouts expose manufacturing compromises. At Fortune, 30 years of engineering expertise means we do not act as passive order-takers or simply modify standard catalogs. We engineer custom inflation solutions from the chemical formula up. You do not need to provide perfect CAD sketches—just bring us your specific fitment challenges and performance limits. Our dedicated engineering team will take over, executing a definitive four-stage OEM workflow that seamlessly scales your custom valve stems from initial material diagnostics to defect-free mass production strictly on schedule.
01
A generic tubeless stem or inner tube valve cannot accommodate every custom alloy rim or severe heavy-duty environment. Instead of asking you to fill out a spec sheet, our engineering team diagnoses your specific operational challenges to formulate the exact solution:
If your custom alloys suffer from tight brake clearances or unconventional rim thicknesses, we calculate precise bend angles and exact base collar dimensions (e.g., Ø8.3mm, Ø11.5mm, Ø16mm) to guarantee flawless, zero-leak TPMS integration. For tube-type applications, we calculate the optimal vulcanization base pad diameter to ensure seamless inner tube bonding.
Tell us your target environment, and our in-house chemists will formulate the polymer. We match high-tensile HPb59-1 brass or lightweight aluminum to your load requirements, and select the exact rubber compound—EPDM for severe UV/ozone resistance, Natural Rubber for optimal tube bonding, or Viton for specialized chemical exposure.
For fleets operating across extreme temperature bandwidths (from -40°C Arctic cold to +130°C continuous heavy-hauling heat), we structurally reinforce the internal brass core wall thickness—upgrading from the standard 0.8mm to a heavy-duty 1.2mm—to completely prevent high-pressure thermal deformation. Simultaneously, we precisely calibrate the EPDM Shore A vulcanization hardness to exactly 65±5. This specific formula guarantees the stem remains pliable enough for rapid pneumatic tool installation (requiring <450N of pull-in force), while maintaining high-speed anti-extrusion rigidity capable of resisting over 600N of blowout force at continuous 100 PSI loads.
02
Before cutting any tooling metal, we eliminate manufacturing risks in the digital space. We run advanced 3D thermodynamic mold-flow simulations (such as SIGMASOFT®) on your custom wheel stem design. This digital validation predicts exact rubber distribution and curing temperatures down to the second, completely preventing internal porosity or exterior rubber flash (burrs) while ensuring optimal molecular cross-linking density. Once digitally validated, our 5-axis Swiss-type CNC centers produce exact-tolerance (±0.01mm) brass core prototypes. We specifically machine the rubber-bonding surface to a precise Ra 0.4 µm roughness to maximize mechanical adhesion, delivering a fully functional custom tire valve for physical fitment testing within a strict 48 to 72-hour window.
03
Your custom prototypes are not approved until they survive our destructive testing lab. We do not guess on safety margins; we benchmark your custom tire schrader valve against strict SAE J1205/J1206 and ISO 14960 standards. We simulate your harshest field conditions through 72-hour high-concentration ozone chamber testing (50 pphm at 40°C) and dynamic fatigue testing, subjecting the stem to 10,000 continuous 25° bending cycles. We mandate 150 PSI hydrostatic burst tests for the metal housings, over 600N of direct axial pull-out force on precision tensile testers, and zero-tolerance micro-leak validation (< 10⁻⁶ atm cc/s). We only grant final engineering sign-off when the prototype proves it will never dislodge or degrade under severe radial loads.
04
Upon your final prototype approval, we initiate permanent multi-cavity mold fabrication using high-grade S136 hardened tool steel (engineered for a lifespan exceeding 500,000 vulcanization cycles), completing custom tooling within a strict 15 to 25-day window. As your custom bolt in valve stems or heavy-duty snap-in units enter our 250-ton automated vacuum vulcanization presses, we maintain zero-defect batch consistency (maintaining a CPK > 1.33) through 100% Automated Optical Inspection (AOI). Every single unit is optically scanned by high-resolution sensors to verify flawless 0.305″-32 thread pitches and perfect rubber-to-metal bonding, ensuring your assembly lines receive commercial-grade safety precisely on schedule with defect rates strictly capped under 50 PPM.
For 30 years, Fortune has operated strictly as a direct source manufacturer of automotive tire valves. We do not outsource assembly. We physically own and control the entire production infrastructure within our ISO/TS16949-certified facility. By integrating in-house EPDM rubber compounding, imported German and Japanese CNC machining centers, and 100% automated pre-shipment leak testing lines, we control every manufacturing variable. Supported by direct Ningbo Port export logistics, we execute high-volume, zero-defect mass production backed entirely by hardware assets and certified data.
30 years of specialized tire valve manufacturing with zero outsourced assembly, maintaining a fully integrated in-house operation spanning R&D, rubber compounding, and CNC machining.
Strict adherence to ISO/TS16949 automotive quality management and verified TUV/DOT product standards, ensuring fully traceable compliance for global markets.
Deployment of automated production lines and imported German and Japanese CNC equipment to guarantee micron-level dimensional accuracy and absolute batch consistency.
Dedicated engineering support utilizing in-house tool and die centers to rapidly translate custom specifications into functional prototypes within 48 to 72 hours.
Mandatory leak, burst, and durability testing on every single outgoing unit, physically eliminating defective parts to protect your assembly lines from warranty risks.
Independent material formulation using virgin EPDM rubber and high-tensile brass to deliver extreme resistance against thermal expansion, ozone, and high-speed radial stres
Comprehensive manufacturing capacity covering snap-in, clamp-in, TPMS, and heavy-duty truck valves, providing one-stop sourcing for all vehicle categories.
Strategic manufacturing localization anchored directly in Ningbo, backed by VCI anti-oxidation packaging and robust international shipping infrastructure.
Acorn lug nuts that are not tightened to the correct torque can cause a wheel to come loose at highway speed — one of the most dangerous failures a driver can experience. Too loose, and the wheel works free over the first 100 km; too tight, and the studs stretch
Lug nuts with incorrect torque can cause a wheel to come loose at highway speed — one of the most dangerous failures a driver can experience. Too loose, and the wheel works free over the first 100 km; too tight, and the studs stretch or snap under load. The fix
A wheel comes off the balancer with a 0.25 oz imbalance marked at the 6 o’clock position. The operator cleans the spot, presses on an adhesive wheel weights strip, watches the display drop to zero, and rolls the wheel to the mounting rack — only to find the weight sitting
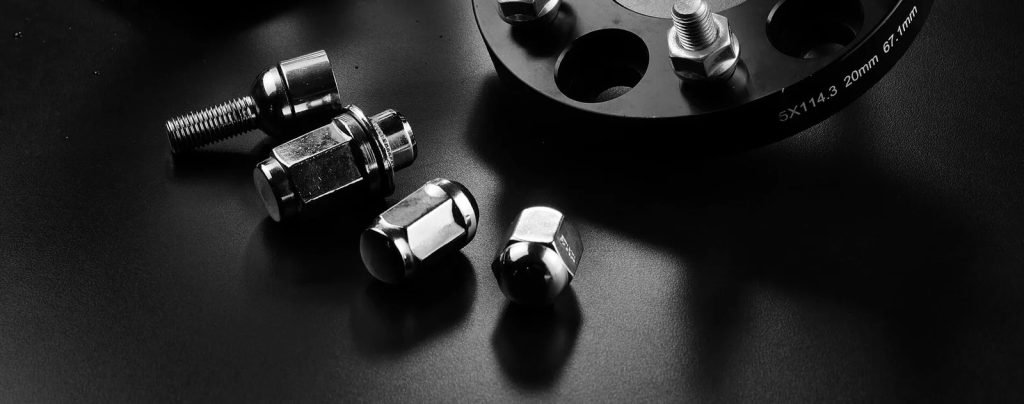
The stock wheel nuts on most cars do their work without anyone noticing them — until the day a wheel wobbles, a stud snaps, or a finish gets scratched during a tire swap. Aftermarket lug nuts solve the cosmetic problem but introduce a technical one: every wheel and stud combination
Fortune tire valves are manufactured under strict quality management systems and comply with international automotive industry standards. Our products are available with certifications and testing requirements such as ISO 9001, IATF 16949, DOT, and TUV depending on product models and customer requirements.
For standard tire valve products, the MOQ is usually 1,000 pieces per model. For customized products, including private labeling, special specifications, or new designs, the MOQ may vary depending on tooling, materials, and production requirements. Our team will confirm the best MOQ based on your project details.
Yes. We provide customized packaging solutions according to customer requirements, including private labels, product labels, cartons, and packaging designs. This helps distributors build their own brands and improve market competitiveness.
Yes. Fortune can provide samples for quality evaluation and compatibility testing before mass production. Customers can verify product performance, specifications, and packaging requirements before placing large orders.
For standard tire valve products, the typical lead time is around 15–25 days after order confirmation. For customized products, including special specifications, new tooling, or private labeling, the lead time is usually 30–45 days depending on project requirements. For urgent orders, Fortune can discuss expedited production options based on capacity and material availability.